Push-Down Forging Press
A hydraulic press for hot open-die forging, offered in two-column and four-column arrangements.
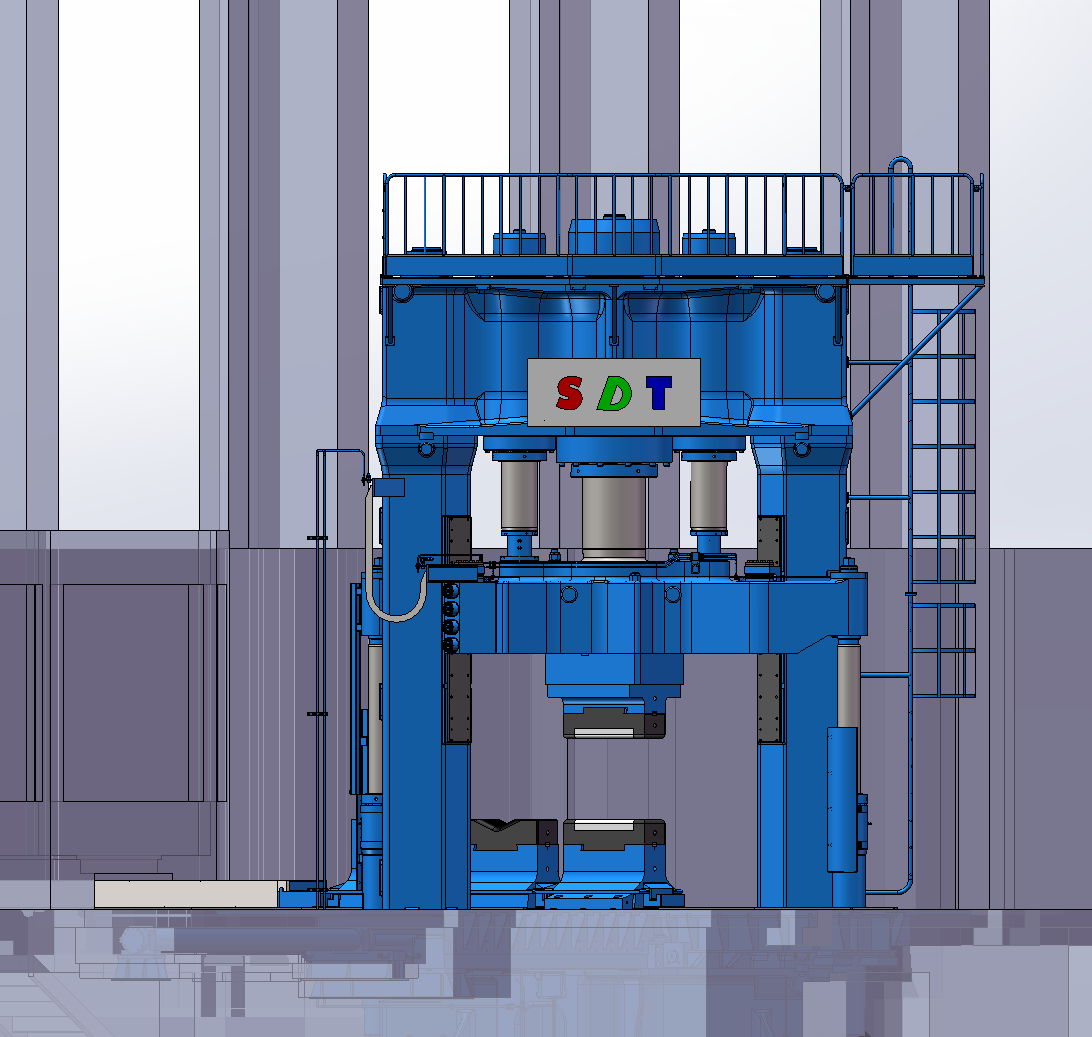 Engineering visualization
Functions and application.
SDT push-down forging presses form heated ingots and billets through operations including upsetting, drawing out, punching, ring expansion and cutting. Appropriate tooling enables the production of bars, discs, rings and thick plate forgings.
The catalogue identifies two-column and four-column structures. The downward pressing arrangement and the available die space are matched to the forging task. Press force, upper-die stroke, daylight, clear width between columns and table dimensions define the main working envelope; handling-machine and tooling interfaces are specified for the installation.
Forming operations
Supports open-die processes with tooling selected for the required forging.
Two-column / four-column options
The arrangement is selected for working-space and installation requirements.
Relevant material families
Material families include carbon, alloy and stainless steels, tool steels and non-ferrous materials such as titanium and niobium alloys.
Technical overview.
- Series reference
- 20 / 25 / 31.5 / 45 / 63 / 80 MN
- Working-space parameters
- Upper-die stroke, daylight, column clearance and table dimensions
- Additional specification parameters
- Table shifting, die shifting, power, forging speed and frequency
- Tooling and handling interfaces
- Specified for the forming process
The selected series and specification depend on the workpiece, material, tooling and required forging operation. Model values are confirmed in the project specification.
Project inputs and application context.
Define the forming task, working space and push-down arrangement.
Discuss the equipment around your real production conditions.
Share an RFQ, drawing, layout or short description. SDT will coordinate the next technical discussion.
Discuss Your Project