Furnace approach
Opening size, sill height, access direction and required reach define the machine-to-furnace interface.
 Discuss Your Project
Move hot workpieces between the furnace and the next process position along a defined or variable route.
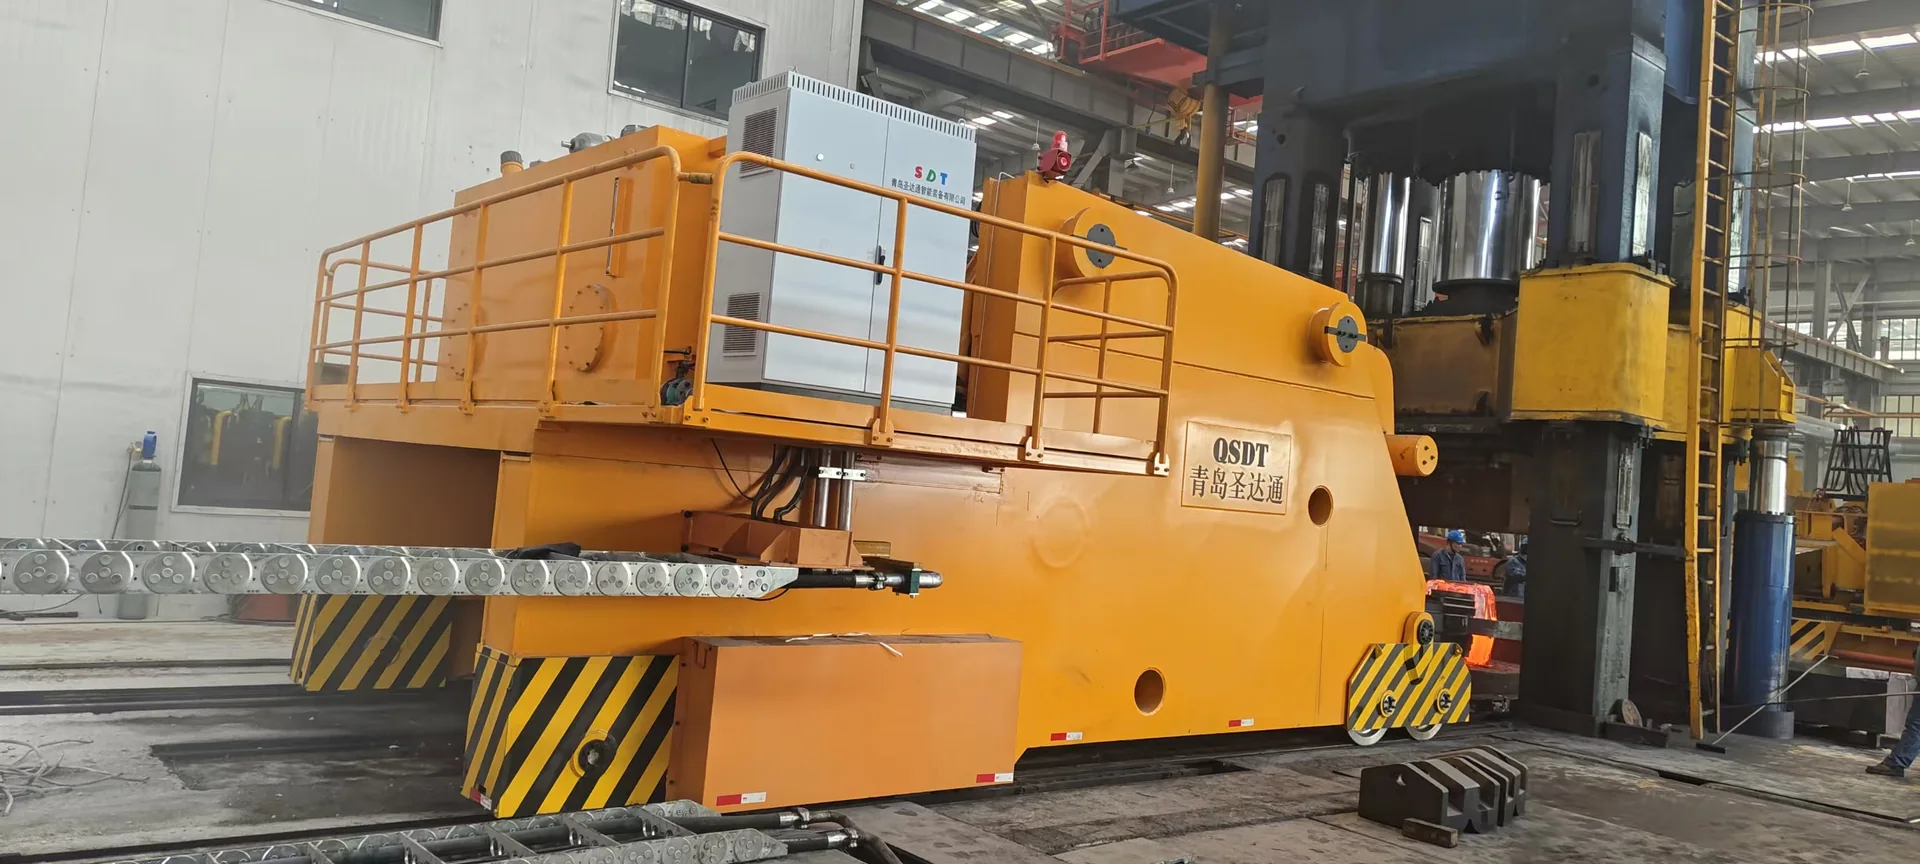
Furnace opening, charging depth, support points and the path to the next process position determine which charging architecture is practical.
Opening size, sill height, access direction and required reach define the machine-to-furnace interface.
Origin, destination, travel distance, turning space and floor or rail conditions define the movement path.
Rail-bound, purpose-built mobile and forklift-based machines answer different route and platform conditions.
Engineering focus
A rail-bound machine suits a defined route and repeatable alignment. A purpose-built mobile machine serves variable positions. A forklift-based solution depends on an engineered platform, attachment and load-center responsibility.
SDT will review the equipment requirement and coordinate the next technical discussion.
Discuss Your Project